-
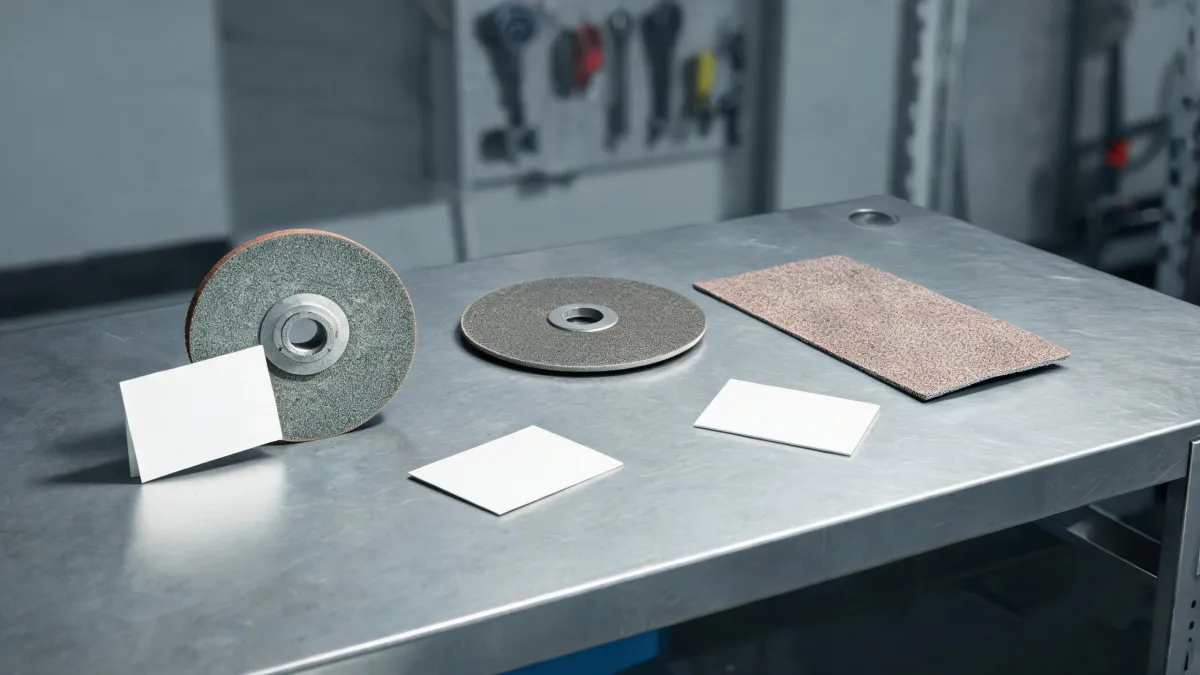
There's No One "Best" Norton Abrasives Wheel
-
Scenario 1: Toolroom Precision Grinding — 38A220-HVBE
-
Scenario 2: Production Cut-Off and Heavy Fabrication — BlueFire R821P
-
Scenario 3: General Angle Grinder Work — Grinding Wheel 71897
-
Scenario 4: Maintenance and Repair — Know Your Material First
-
How Do You Know Which Scenario You're In?
-
The Price Trap I Keep Re-Learning
There's No One "Best" Norton Abrasives Wheel
I've been ordering abrasives for our fabrication shop since 2017. In that time, I've personally made—and documented—eight significant mistakes, totaling roughly $4,700 in wasted budget. Now I keep our team's checklist so nobody repeats them (unfortunately, some of those lessons came with a hard price tag).
The question I get most from new hires and even some distributors is which Norton abrasives product they should be using. It's the right question, but it has no single answer. The best pick depends on what you're doing. Here are the four scenarios I've classified over the years:
- Toolroom precision grinding → Norton abrasives 38A220-HVBE
- Production cut-off work → Norton abrasives BlueFire R821P
- General angle grinder work → Norton grinding wheel 71897
- Maintenance and repair → depends on the material
Let's walk through each one.
Scenario 1: Toolroom Precision Grinding — 38A220-HVBE
If you're sharpening tool bits, grinding hardened die steel, or holding a finish measured in tenths, you're in toolroom territory. The Norton abrasives 38A220-HVBE is the one I reach for.
Breaking down the name helps. 38A is Norton's premium white fused aluminum oxide grain. It's friable, meaning it fractures at a microscopic level and presents fresh cutting edges instead of loading up or glazing. The 220 is the grit size. HVBE is a vitrified bond formulated for precise, controlled stock removal. It's the sort of wheel that makes a surface grinder behave like a much more expensive machine.
My mistake in this scenario goes back to late 2017, my first year on the job. I ordered a cheaper "universal" wheel because the 38A220-HVBE was roughly twice the price. The universal wheel worked for the first few passes. Then it glazed over, generated enough heat to burn the workpiece, and we had to rework a $600 die component. That cost $600 plus a two-day delay, all to save perhaps $80 on a wheel.
If I could redo that decision, I'd order the 38A220-HVBE every time. The price difference disappears the moment you factor in rework rates.
Scenario 2: Production Cut-Off and Heavy Fabrication — BlueFire R821P
Different job, different priorities. If you're cutting bar stock, pipe, or structural steel—especially stainless—in production runs, cutting speed and consistency are what matter. That's where Norton abrasives BlueFire R821P cut-off wheels shine.
I remember our first head-to-head test in March 2023. A senior welder had used BlueFire at his previous shop and brought a couple in. We timed cuts on 2-inch schedule 40 pipe, four cuts each against the brand we'd been using. The R821P averaged 22% faster per cut. Not slightly faster—a full fifth of our cutting time gone.
Even after that test, I hesitated to switch our stock. What if the results were a fluke? We ordered a single case, ran it for a week, and tracked every cut. The numbers matched. It took another month before I fully stopped second-guessing the purchase.
Now, the price elephant. The BlueFire wheels cost more per wheel. A 200-piece order came out about $140 higher than the alternative. That might look like a reason to save, but I learned that lesson the hard way in 2022, when I ordered 200 budget cut-off wheels from a distributor I'd never used. The crew went through more than half in the first month. Cutting was slower, burrs were worse, and several wheels wore down to the center before half their expected life. The $240 I saved "on paper" turned into $510 in replacement wheels plus extra labor hours. I still kick myself about that one.
Value over price isn't a slogan. It's arithmetic.
Scenario 3: General Angle Grinder Work — Grinding Wheel 71897
Now for the job that fills most of a fab shop's day: grinding welds flush, cleaning scale, beveling edges. For this mixed work, the Norton grinding wheel 71897 is the practical pick. It's a Type 27 depressed-center wheel that handles mild steel, aluminum, and occasional stainless without any special setup. It's not exotic. It just works.
And this is where the question I hear more than any other shows up: "which way does angle grinder blade go?"
I don't mock the question, because I've installed cut-off wheels backward twice—once in 2018 and once in early 2022. Both times, vibration and slow cutting tipped me off before anything failed. But that's not a strategy.
If the wheel has an arrow printed on it, that arrow points in the direction of spindle rotation. There's almost always a matching arrow molded into the grinder's guard. Line them up before tightening the arbor nut.
Flap discs are a slightly different case. Most have directional arrows too, and installing one backward means the flaps hit the work surface at the wrong angle—it feels like you're sanding with a brick. One of our apprentices tried to mount a flap disc with the label facing the grinder body on his third day. A welder caught it before he powered up.
Also worth checking while you're at it: the maximum RPM rating stenciled on the wheel. In 2019, I matched a wheel rated for 6,600 RPM to a grinder running 8,500 no-load. It held (thankfully), but it was loud, unbalanced, and left a poor finish. The rating on the side isn't a suggestion.
Scenario 4: Maintenance and Repair — Know Your Material First
Here's a scenario that's come up more often in our shop over the last couple of years: maintenance jobs on pumps and rotating equipment. If you're rebuilding a centrifugal pump, replacing a shaft, or cleaning up a seal face, the right abrasive depends on the alloy you're working with—not the one you guess from the part's appearance.
How do you identify it? Get the spec sheet. In many cases, that means searching for the centrifugal pump catalogue pdf from the manufacturer to confirm the shaft material, hardness, and coatings. Removing a worn pump shaft goes differently if it's 304 stainless, 4140 alloy, or a hardened martensitic stainless.
My own miss: I once assumed "pump shaft equals stainless" and reached for a stainless-specific cut-off wheel. The shaft turned out to be 4140 chromoly. The wheel removed the material, but at maybe a third of the speed it should have, and I burned through two wheels instead of one. Not catastrophic—just a reminder that material identification comes before wheel selection.
For light seal face cleaning, the 71897 is usually fine. If you're dressing down a hardened shaft, you'll do better with a toolroom-style wheel from Scenario 1. For cutting pump piping, the BlueFire R821P is the right choice.
How Do You Know Which Scenario You're In?
If you're still unsure, ask yourself three questions.
- What's the tolerance? If the surface finish or dimension has to hold tight, you're in Scenario 1 territory. If it's general removal and cleanup, you're in Scenario 3.
- What's the material, and how much of it? Production stainless cutting all day points to Scenario 2. A one-off repair on a pump points to Scenario 4.
- Which variable matters most—cutting speed, finish, or wheel life? The BlueFire R821P optimizes for speed. The 38A220-HVBE optimizes for finish and control. The 71897 is the balanced all-rounder.
And if you're genuinely stuck, call your Norton distributor. Give them the material, the machine, and the RPM. They'll sort it out.
The Price Trap I Keep Re-Learning
It's tempting to think a grinding wheel is just a grinding wheel—pick the cheapest one and move on. From the outside, the budget wheel looks like the rational purchase. The reality: wheels differ in speed, life, finish, and safety. The lowest unit price looks good on a spreadsheet, but abrasive cost is a small fraction of the total cost of grinding. Labor dominates. A wheel that's 15% cheaper but 20% slower is a bad trade.
I'm not saying buy the most expensive option blindly. I'm saying calculate cost per completed cut, not cost per wheel. The BlueFire test wasn't about brand loyalty. It was about which wheel does the job at the lowest total cost.
Norton is the brand I keep returning to because the product line covers these scenarios and the spec sheets are consistent. But the brand isn't the point. Matching the wheel to the job—and installing it the right way—is the point.
Check the arrow. Check the RPM. Know your material. And don't let a cheap price lure you into an expensive rework.
Maren Jorgensen
Maren Jorgensen is an independent hand tool and torque applications analyst covering wrenches, pliers, screwdrivers, hammers, sockets, ratchets, hex keys, and tool sets. She applies ISO 6789-1 torque-tool conformance principles while examining jaw capacity, leverage, fastener engagement, torque range, accuracy, handle geometry, and material hardness. Her practical guides help tradespeople and procurement teams select suitable tools, plan controlled tightening, and compare durability without relying on brand reputation alone.