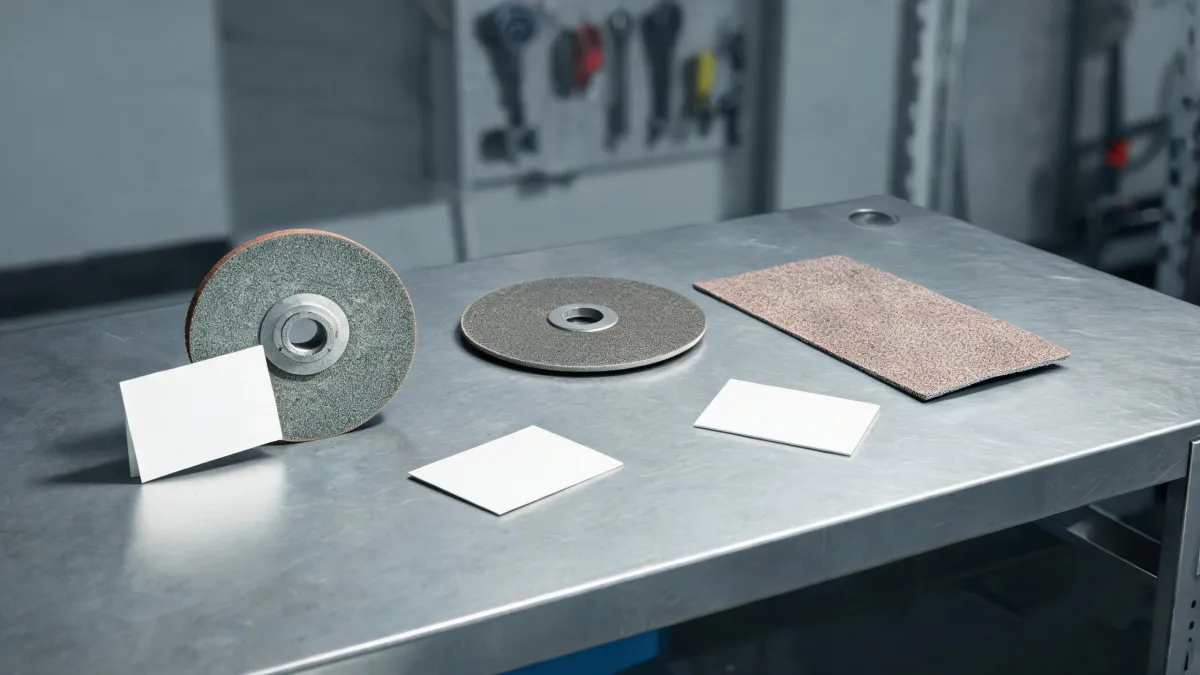
If you manage purchasing for a metalworking operation, you have probably heard this question: which Norton abrasives should we get? I sit on the buying side. For about six years, I have handled abrasives procurement for a mid-sized fabrication shop, tracking every order in the same cost sheet - roughly $16,000 to $18,000 a year, depending on backlog. After watching what actually gets consumed on the floor, I have stopped giving one standard answer. There are three different situations, and they call for three different buying strategies.
First: make sure it is actually Norton
Boring but necessary. If you search for the phrase norton abrasives trademark owner saint-gobain, you will find the ownership structure quickly: Norton Abrasives is a Saint-Gobain brand. For a buyer, that means there is a formal distribution channel and a company standing behind the product. We bought Norton-style wheels once from a marketplace seller. The printing looked close enough. The safety data sheet did not exist.
The official Norton site has a where-to-buy locator, and that is where I start when we open an account at a new facility. It lists Norton abrasives distributors that are authorized to sell the real product. A genuine wheel should also carry clear markings: wheel type, arbor size, and maximum RPM. Any wheel meant for a 4-1/2-inch angle grinder will show that information. The grinding wheel safety standard we follow at our shop is ANSI B7.1, and the simplest rule from it is never operate a wheel above its rated speed. If the label is missing or faded, do not mount it. Return it.
Scenario 1: the grinder is one tool in the toolbox
If your 4-1/2-inch angle grinder gets used for an hour here and there, and you go through fewer than 25 wheels a month, you are in the convenience category. You do not need a procurement contract. You need a distributor that stocks what you use and is close enough to reach during a lunch break.
Find a local authorized dealer, ideally one with a counter and someone who actually knows abrasives. Bring in your old wheel or write down the part number. For occasional work, a premium product like a Norton Type 27 grinding wheel tends to be worth it, not because the cheap wheel is always terrible, but because your real cost is the trip to the store when a wheel fails halfway through a job.
Do not buy a case of 100 generic wheels just because the per-piece price looks good. Fifteen wheels a month means that case will sit in storage for a while, and storage conditions matter for resin-bonded wheels. I have seen old stock get brittle. The savings disappear the first time a damaged wheel throws a chunk.
Scenario 2: you are burning through wheels every shift
Once you are north of, say, 100 wheels a month, the game changes. You are no longer buying a product. You are buying uptime, consistency, and predictable cost per cut. In this scenario, random online ordering will burn you eventually.
Set up a formal account with one of the Norton abrasives distributors in your region. Ask them to stock the specific sizes you use and give you a 12-month price sheet. We did this two years ago, and it cut our procurement time more than it cut our product cost. The price per wheel was maybe 4 percent lower. The real savings was not having a maintenance tech waiting three days for a restock.
This is also the scenario where you need to match the wheel to the work. A cutoff job on thin stainless sheet is a Type 41 or Type 42 cut-off wheel job, not a grinding wheel job. Heavy weld removal is a different product again. We log test cuts for any new wheel we evaluate. Ten cuts, count the time, measure the wear, and then compare cost per usable cut rather than price per wheel. A so-called bargain wheel that lasts half as long is not a bargain.
One warning from our own history: if a listing looks like a major brand but the price is suspiciously low, check whether the seller is authorized. We ignored that check once and received a batch that looked right but ran rough. I am fairly sure they were counterfeit. We scrapped the whole case. The few dollars we saved turned into a $600 mistake, and that is not counting the lost time.
Scenario 3: the problem is not an abrasives problem
Not every purchasing request that lands on my desk actually needs an abrasive answer. Last year, someone asked me for more flap discs, but what he really wanted was a way to join thin stainless sheet without warping it. Before long, that request turned into exactly what you would expect: people searching for where can I find a metal laser welding machine.
That is a fair question. A hand-held laser welding machine is a real option for thin sheet work. It is also capital equipment, not a shop consumable, and a good abrasives distributor will not pretend to be your laser systems integrator. The honest answer is usually: talk to a company that specializes in laser welding equipment and has application engineers who can run your parts.
The vendor who told us this is not our strength, and here is who does it better, earned our trust for everything else.
Do not let a supplier sell you a grinding solution when the process itself is wrong. If you want to eliminate a finishing step, changing the weld process may be the real fix. That is not a failure of the abrasive supplier. That is a supplier respecting the boundary of their expertise.
Spindle threads, arbor holes, and the grinder nut
Even when you buy the right wheel, mounting problems can create the exact issues you were trying to avoid. The 4-1/2-inch angle grinder category is mostly 115 mm wheels with a 7/8-inch arbor hole in North America. Spindle threads are commonly 5/8-11, but some imported grinders use M14. That is where the grinder nut becomes important.
The grinder nut is the clamping part that holds the wheel on the spindle. It is not a generic piece of hardware. If the nut is rounded, cracked, or replaced with the wrong thread pitch, the wheel will not sit flat. A wheel that runs out will vibrate, cut poorly, and put unnecessary stress on the spindle bearings. We keep a spare nut in our tool crib now. It costs a few dollars, and it has saved us more than one frustrating afternoon.
I should add that we never tighten the grinder nut with an impact wrench. Use the wrench that came with the grinder, press the spindle lock, and snug it down firmly. Over-tightening can damage the wheel flange and, in some cases, the wheel itself. If you are not sure whether a wheel is compatible with your grinder's thread or arbor, bring the grinder nut to a local distributor and compare threads before you buy in bulk.
So which one are you?
If you are still unsure, answer these three questions honestly:
- Do you use fewer than 25 wheels a month? Follow scenario 1. Buy locally, buy small quantities, and do not overthink the inventory.
- Do you use multiple boxes of wheels per week? Follow scenario 2. Build a stocking relationship with an authorized distributor and track cost per cut, not cost per wheel.
- Is your real question about joining sheet metal or removing weld seams faster? Follow scenario 3. Start asking about laser welding equipment integrators or a process change, not about the next box of abrasives.
The most expensive abrasive I have bought was not the most expensive one on the invoice. It was the wheel that failed mid-cut, damaged the part, and forced a redo. After six years of tracking every order, I have come to believe that the brand matters less than the fit between the product and your actual workflow. When you get that fit right, Norton abrasives are easy to justify. When you do not, no brand name will save you.
Maren Jorgensen
Maren Jorgensen is an independent hand tool and torque applications analyst covering wrenches, pliers, screwdrivers, hammers, sockets, ratchets, hex keys, and tool sets. She applies ISO 6789-1 torque-tool conformance principles while examining jaw capacity, leverage, fastener engagement, torque range, accuracy, handle geometry, and material hardness. Her practical guides help tradespeople and procurement teams select suitable tools, plan controlled tightening, and compare durability without relying on brand reputation alone.