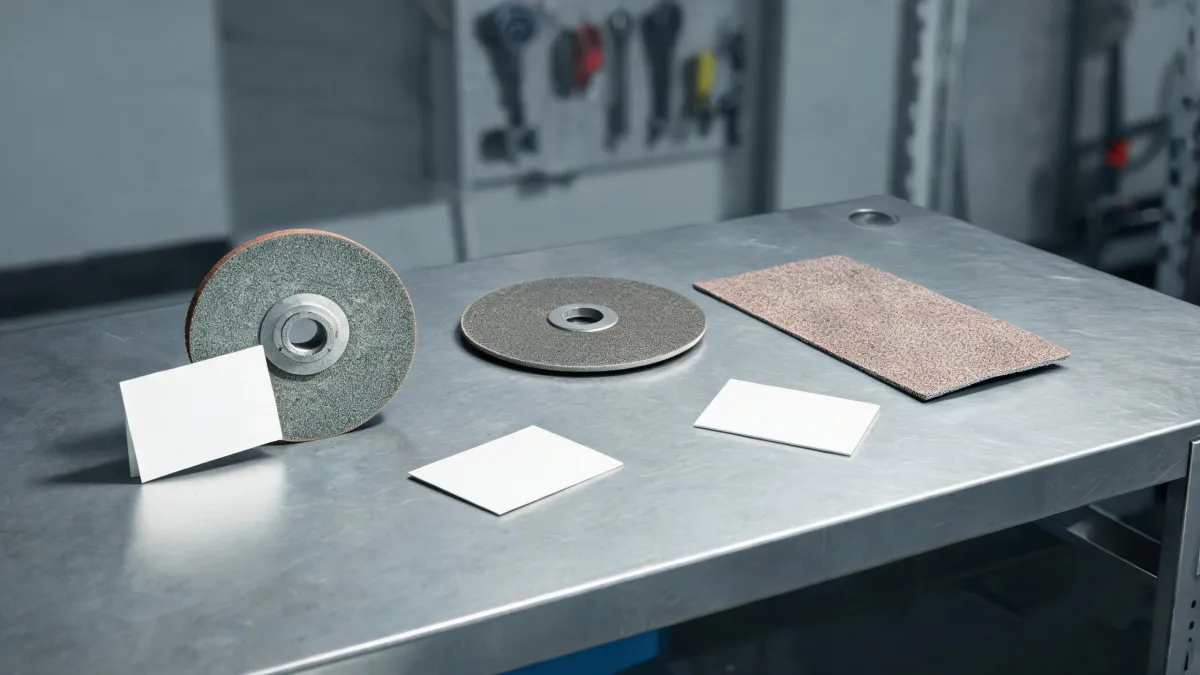
Let's say you're in the middle of a quick workshop job—maybe you finally searched 'how to take off caster wheels' and you're ready to swap them on an old workbench. You reach for your 18V angle grinder, grab whatever disc is lying around, and start cutting. Halfway through the first wheel, the disc is gone. Not worn out—like, literally disintegrated.
You drive to the hardware store (again), buy another pack, and finish the job an hour later than planned. Annoying, but no big deal, right?
Wrong. That one bad disc can be the difference between a profitable job and a money pit. In my role coordinating abrasives for maintenance crews and contractors, I've handled 200+ rush orders over the past five years—from plant shutdowns to same-day replacements for food processing lines. This exact scene plays out daily.
The Surface Problem: 'This Disc Is Junk'
When I first started in this industry, I assumed that when a grinding disc failed, it was just a cheap product. Period. I'd hear customers say, 'Norton is overpriced; the no-name disc from the auto parts store does the same job for half the price.'
Honestly, I get it. Nobody likes paying more for a consumable. But after three budget overruns and a lot of overtime, I realized the problem isn't the brand. It's that most people are using the wrong disc for the material in front of them.
Actually, let me back up. That's the surface issue. The deeper problem is how we think about abrasives in the first place.
The Deep Cause: You're Fighting the Material
A grinding disc isn't a magic eraser. It's a cutting tool with a specific grain, bond, and geometry, engineered for a narrow range of applications. Use it outside that range, and it will fail—fast.
Reason #1: You're using a metal disc on masonry (or vice versa)
The classic example in our warehouse: someone grabs a 'Type 27' disc and assumes it's universal. But Type 27 just describes the shape—depressed center, the standard flat grinding disc. A masonry grinding disc type 27 is designed for concrete, brick, and block. Use that same wheel on a steel bolt (like the one holding a caster wheel in place), and the bond that's meant to break down on masonry will crumble on metal. It'll wear out in minutes. Worse, it can shed material unevenly, which at 8,000+ RPM is a safety hazard.
When someone calls and says their disc 'melted' trying to cut a steel pin, my first question is: what material was the disc rated for? Nine times out of ten, it's the wrong family.
Reason #2: The grain technology doesn't match your tool
Here's the part most buyers miss. Standard aluminum oxide grain is basically crushed rock with a binder. It starts sharp, but it dulls fast. The friction slows the cut and generates heat. That heat breaks down the bond, which makes the problem worse. It's a vicious cycle.
Higher-performance discs, like Norton Abrasives BlueFire R821P, use ceramic aluminum oxide grain. Ceramic grains fracture at a microscopic level as they work, exposing fresh sharp edges. Instead of going dull, the disc keeps cutting. The practical result: faster material removal and a visibly shorter job—not just a 'longer lasting wheel.'
(And before you ask: no, this isn't a marketing-gimmick 'nano grain' pitch. The mechanism is well documented in abrasives engineering. It's the same reason ceramic grinding wheels cost more than the brown ones—and why they end up costing less per cut.)
Reason #3: The tool isn't running at the speed you think it is
An 18V angle grinder is convenient, but it doesn't perform like a corded 4-1/2-inch grinder. Most 18V grinders spin at about 8,500 RPM no-load (some lower), while corded models can hit 10,000–11,000 RPM. A wheel engineered to bite at 10,000 RPM will just skid or glaze at 8,500.
Two things matter here. First, the wheel's rated speed printed on the blotter must be higher than your grinder's max RPM. That's non-negotiable, per ANSI B7.1. Second, you need a disc that actually performs at the speed your tool delivers—not the one on the box.
Per ANSI B7.1, the operating speed of a grinding wheel must never exceed the maximum operating speed marked on the wheel. Verify current requirements at the official ANSI source.
I remember a facility manager in March 2024, 36 hours before a major shutdown window, who called because his crew had gone through 60+ cheap discs in two days on an 18V grinder. The job was supposed to take one day. It was looking like two. He didn't need another discount vendor; he needed a wheel with grain that kept cutting at lower speeds.
The Cost Nobody Counts
Now we get to the part nobody wants to hear: total cost of ownership.
Let's say a budget disc costs $3 and stops cutting after 15 minutes. A premium disc costs $8 and lasts 45 minutes of actual cutting. Per minute, the budget disc is actually more expensive—$0.20 vs $0.18—and that's before you factor in the cost of stopping work to change the disc, standing around, and rework from a glazed wheel that's burning the steel instead of cutting it.
Break it down:
- Disc cost per minute: $0.20 (budget) vs $0.18 (premium)
- Time to change a disc: 3–5 minutes, if the operator is quick
- Time to drive to the store when a disc fails: 30–60 minutes
- Rework after a bad cut: hours, or the whole part
I want to say the exact price gap was $5 per wheel, but don't quote me on that—your distributor will have current numbers as of April 2025. The point is the math doesn't work in favor of 'cheap' discs.
Last quarter alone, we processed 47 rush orders for customers who ran out of abrasives mid-job. These orders ranged from a single $50 wheel to a $15,000 pallet order. Most had one thing in common: they bought on price per disc, not cost per finished cut. One customer who bought 100 cheap wheels at $2.50 each ended up spending $300 in extra labor to fix what those discs did to his steel.
Then there's the shutdown job in March 2024. A facility manager called 36 hours before a locked maintenance window. His crew had burned through 60+ cheap discs in two days on an 18V grinder. The window couldn't move—missing it meant a $50,000 penalty clause. Normal delivery for a case of the right wheels was three days. We found a way to get BlueFire wheels to him overnight, paid $180 in freight, and the crew finished with hours to spare. Our internal policy now requires a 48-hour buffer on any shutdown job.
That's the $300 mistake. Not the disc—the thinking.
Now, to be fair, the $8 disc isn't always the right answer. For a one-off job that takes two minutes, a cheap disc is fine. The TCO argument is about production work, where you're grinding for more than 10 minutes at a time. If you're doing one cut to remove a caster wheel, use whatever you have—but know that a glazed disc on a stuck bolt is how people end up throwing an 18V grinder across the garage. Let's keep the math simple: if it takes you more than 15 minutes to finish a 5-minute job, the disc wasn't cheaper.
The Fix: Match the Wheel to the Work
Now for the part that matters. The solution isn't 'buy the most expensive Norton wheel you can find.' It's using the right wheel for the material, the tool, and the job.
For metal grinding on an 18V grinder
If you're grinding weld seams, removing rust, or knocking the head off a steel bolt to free a caster wheel, you want a Type 27 wheel with ceramic grain. The Norton Abrasives BlueFire R821P is a solid example. It's designed for high-pressure grinding and holds up at the lower end of the RPM range where 18V grinders live.
The SKU I see most often in our warehouse orders is Norton Abrasives 63642543463—a Type 27 BlueFire R821P wheel. (Double-check the dimensions on the box before ordering; Norton makes several sizes in this series.)
For masonry
Cutting concrete or brick? Don't reach for a metal grinding wheel. You need a masonry grinding disc type 27 that's rated for masonry. The label will say it. Use it only on masonry, and let the wheel do the work—extra pressure just shortens the disc's life.
The 30-second check before any cut
- Look at the material. Is it metal, masonry, or something else?
- Look at the wheel label. What material is it rated for?
- Look at your grinder. Does its max RPM exceed the wheel's rated speed?
Answer all three correctly and you've eliminated 80% of premature disc failures. The rest is technique—and that's on you.
Bottom Line
Grinding discs don't fail in isolation. They fail because of a mismatch between the disc, the material, and the tool. That mismatch costs more than the price of a new disc—it costs time, rework, and sometimes the whole job.
I'm not going to tell you Norton Abrasives is the only brand worth buying. What I'll tell you is this: when a customer calls with a real emergency and needs a wheel that won't quit, the BlueFire R821P is what we grab. For the price of one decent wheel, you might save yourself a trip to the hardware store—and the $300 mistake.
Now go get that caster wheel off. Properly.
Maren Jorgensen
Maren Jorgensen is an independent hand tool and torque applications analyst covering wrenches, pliers, screwdrivers, hammers, sockets, ratchets, hex keys, and tool sets. She applies ISO 6789-1 torque-tool conformance principles while examining jaw capacity, leverage, fastener engagement, torque range, accuracy, handle geometry, and material hardness. Her practical guides help tradespeople and procurement teams select suitable tools, plan controlled tightening, and compare durability without relying on brand reputation alone.