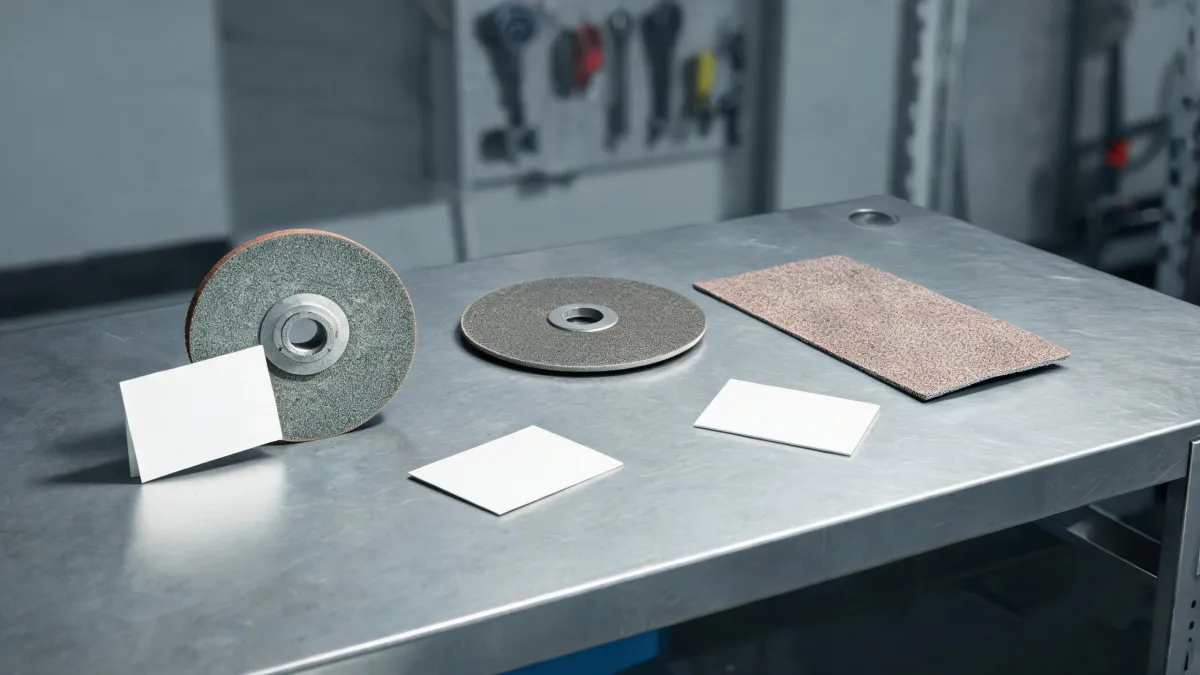
The Short Answer
Buy the $4.20 Norton wheel, not the $1.80 import. Over six years and roughly $180,000 in tracked abrasive spending, the "cheap" option cost us 23% more per finished cut once I counted wheel changes, rework, and idle time.
That's the whole point. Everything below is just me showing my work.
I'm a procurement manager at a 120-person metal fabrication shop outside Pittsburgh. I've owned our consumables budget for six years, negotiated with 40-plus suppliers, and logged every invoice in our cost tracking system since 2019. When I say 23%, it isn't a guess. It's what came out of the spreadsheet after Q2 2024.
Here's the thing: I didn't start out believing this. I started out believing the opposite.
Why I Used to Buy the Cheap Stuff
Everything I'd read about procurement said the same thing: commoditize, standardize, and let price decide. Abrasives looked like the perfect commodity. A 4-1/2-inch grinding wheel is a 4-1/2-inch grinding wheel, right? Same arbor size, same thickness, same job.
In practice? That's wrong. Not slightly wrong — meaningfully, expensively wrong.
In early 2023, I ran a comparison. Vendor A quoted $4.20 per Norton wheel on a 500-piece order. Vendor B quoted $1.80 for a generic import with "comparable specs." I almost went with B. On paper, that's a $1,200 annual saving. My director would've been happy.
Then I did the TCO math I should've done from day one.
- Vendor B's wheels wore out roughly 2.4x faster on our 14-gauge stainless work.
- We burned through 3 extra wheels per shift on average — that's operator time, not just product cost.
- Two wheels in the first month failed mid-cut and scarred a $600 batch of handrail stock.
- One of those failures sent a fragment into a guard. Nobody was hurt. That was luck, not design.
Total cost of the "cheap" trial: about $1,940 in rework, replacement, and downtime. On a $900 order.
They warned me about hidden costs with cheap abrasives. I didn't listen carefully enough. The stainless handrail redo made me a believer.
What Actually Matters When You Spec a Wheel
Let me back up. The reason Norton abrasives products hold up in our shop isn't brand loyalty — it's that the spec sheet actually matches the wheel in the box.
When you're running a 4-1/2-in angle grinder — we standardize on the G12SR4, which most reviews clock around 11,000 RPM no-load — you need wheels rated for at least that speed and matched to your material. The G12SR4 reviews I've read tend to focus on the tool: weight, switch feel, vibration. Fair enough. But after running three different wheel types through ours, I'd argue the abrasive matters just as much as the grinder for cut quality and safety. A $70 tool with a $1.80 wheel is a $1.80 cutting experience.
Here's the thing about speed ratings: a wheel rated at 10,000 RPM on an 11,000 RPM tool isn't a gray area. It's a failure waiting for a Tuesday. Norton's 4-1/2-inch line is rated above what the G12SR4 spins. That's not marketing — that's the bare minimum you should verify before any wheel touches the arbor.
Per FTC advertising guidelines, vendors have to substantiate performance claims like "longer life" or "universal fit." So when a distributor tells you their import is "just as good as Norton," ask for the test data. In six years, I've been shown actual test data exactly twice. Both times, the claims softened considerably.
Cutting Tile With an Angle Grinder — What I Actually Do
We do a fair amount of tile and masonry work for commercial fit-outs, and how to cut tile with an angle grinder is one of those questions where the internet gives you twelve answers and eleven of them assume you're cutting a straight line through soft ceramic.
Real talk: the wheel choice does 80% of the work. A continuous-rim diamond blade, run dry with light passes, will out-cut a turbo blade on porcelain every single time. Norton's diamond blades are what we keep on the shelf for this. Score first, cut in 2-3 passes, and don't push. The operators who burn through blades are the ones leaning on the tool.
What I'd tell anyone budgeting for this work: don't buy the cheapest diamond blade you can find and then wonder why you're buying four of them. One $40 blade that finishes the job beats three $15 blades that chip the edge.
Where the Supplier Actually Matters
Lead time is a line item. It just doesn't show up on the quote.
We used to buy abrasives from a national distributor. Great pricing, terrible emergency response. When an operator blows through the last cutting wheel at 3 PM on a Friday and you've got a Monday delivery, a Norton abrasives supplier in Western Pennsylvania is worth a real premium. We switched to a regional distributor out of the Pittsburgh area three years ago. Per-unit price went up about 4%. Emergency-shipping spend dropped by more than that in the first quarter.
Here's a test I use now when vetting any industrial distributor: pull up their epoxy anchors catalog. Sounds unrelated, I know. But how a supplier organizes a technical product catalog tells you how they organize everything. If the epoxy anchors catalog is a PDF from 2021 with dead SKUs and no current pricing, their abrasive inventory is probably being managed the same way. If it's current, filterable, and has actual stock counts, that's a supply chain you can plan around.
I've also started asking suppliers to mail physical samples before a first order. According to USPS pricing effective January 2025, a First-Class Mail large envelope runs $1.50 — under two bucks to avoid a $2,000 mistake. I'll take that trade every time.
What I Got Wrong Along the Way
Not every cheap wheel is a trap, and I don't want to pretend otherwise.
The numbers said go with the import. My gut said stick with Norton. I went with my gut on that first comparison job — and it turned out the import supplier had a two-week lead time they hadn't mentioned. That was luck, not judgment. I've since built a vendor scorecard so the decision doesn't come down to my gut at all.
The real lesson wasn't "always buy premium." It was "always calculate total cost before you look at unit price." Those are different rules, and I confused them for about two years.
When the Cheaper Option Is Fine
I'll be honest about the boundaries here, because pretending premium always wins is just a different kind of lazy.
If you're doing rough grinding where finish doesn't matter — deburring, weld cleanup on non-critical steel, one-off jobs — a mid-tier wheel is usually the right call. You're not going to see the 23% difference because you're not pushing the wheel hard enough for wear rate to matter.
Also, if you don't have a realistic way to track downtime and rework costs, the TCO argument falls apart. You'll just see higher invoices and assume you're overpaying. Build the tracking first. Then switch.
And if your volumes are under, say, $5,000 a year in abrasives? The effort of running TCO analysis probably costs more than the difference. Buy from a supplier you trust, keep a spare box on the shelf, and spend your time on something that moves the needle.
What I won't do anymore is pretend a $1.80 wheel and a $4.20 wheel are the same product with a different label. Six years of invoices say they aren't. So does the scar on that handrail.
Maren Jorgensen
Maren Jorgensen is an independent hand tool and torque applications analyst covering wrenches, pliers, screwdrivers, hammers, sockets, ratchets, hex keys, and tool sets. She applies ISO 6789-1 torque-tool conformance principles while examining jaw capacity, leverage, fastener engagement, torque range, accuracy, handle geometry, and material hardness. Her practical guides help tradespeople and procurement teams select suitable tools, plan controlled tightening, and compare durability without relying on brand reputation alone.