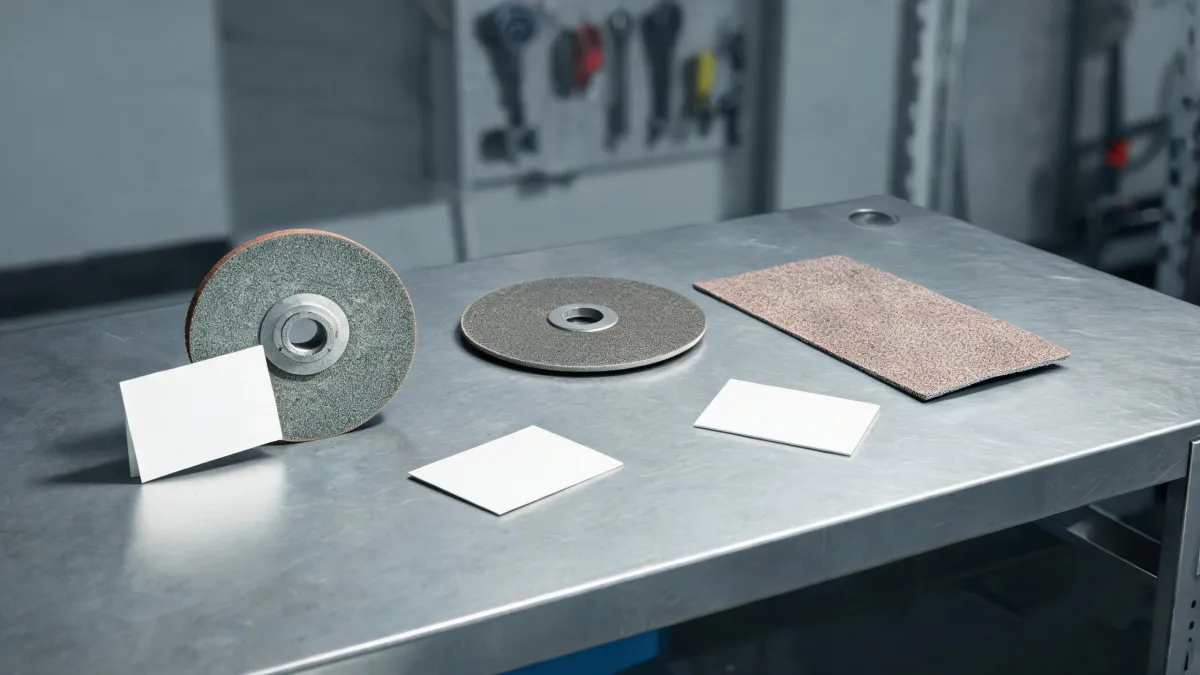
When this checklist applies
I’m the office administrator for a 120-person metal fabrication shop. I manage MRO and tooling orders—roughly $180,000 annually across 11 vendors. I report to both operations and finance. So when someone asks me how to cut aluminum with angle grinder, I don’t start with the cut. I start with what we’re buying, who’s using it, and what happens when the disc is wrong.
This checklist is for maintenance managers, shop supervisors, and admin buyers who order abrasives for a team. It is not a substitute for your tool manual. It is the process I wish we had followed before a simple aluminum trim job turned into a rework ticket.
The 7-step checklist
Step 1: Confirm the aluminum and the cut
Not all aluminum is the same. Extrusion, plate, cast, and thin sheet behave differently. Thickness matters. So does the finish you need. A cut that only needs to be rough is different from a cut that feeds a weld or a visible edge.
Ask the person doing the work three questions: What alloy? What thickness? What tolerance? If nobody can answer, stop. That is the first red flag.
In my opinion, this is the step most buyers skip because it feels like shop work. But if the order is wrong, it becomes my problem.
Step 2: Pick the right abrasive, not just the cheapest disc
Aluminum can load a standard grinding wheel. It gets gummy, overheats, and can create a poor cut or a dangerous wheel condition. You need an abrasive rated for aluminum or a cut-off wheel intended for non-ferrous metal. Check the manufacturer’s application guide.
The Norton Abrasives company, which we tag as norton-abrasives in our purchasing system, publishes speed and application data for its lines. That data is more useful than a marketplace listing that says 'fits angle grinder.'
For finishing and cleanup, we keep norton abrasives polerpads on the shelf for blending. They are not a cutting tool. They are for after the cut, when you need a consistent finish. If your shop also drills mixed metal, the bi- metal hole saw set cmah1set7 is a separate MRO item—don’t confuse it with a cut-off wheel.
One reference SKU we track is grinding wheel 71897. It may be right for some jobs, but verify the wheel diameter, arbor, and max RPM against the grinder before ordering. No SKU is universal.
It took me three years and about 150 abrasive orders to understand that the spec sheet matters more than the invoice discount.
Step 3: Verify RPM, size, and arbor
This is the step that causes the worst problems. The wheel’s maximum RPM must be equal to or greater than the grinder’s no-load RPM. Never use a wheel rated lower than the tool. Never oversize a wheel to get more depth. Never remove a guard just because it is in the way.
Why does this matter? Because a wheel that fails at speed does not fail politely. OSHA 29 CFR 1910.215 and ANSI B7.1 are the baseline references for abrasive wheel safety. As of January 2025, verify current requirements at osha.gov and with your tool and abrasive manufacturers.
I knew I should check max RPM on a rush order, but thought 'what are the odds?' The odds caught up with us when a borrowed grinder had a higher RPM than the disc was rated for. Nobody got hurt. That was luck, not process.
Step 4: Set up the work area and PPE
Before the grinder starts: clear the area, secure the workpiece, and check for flammables. Aluminum dust and sparks can cause problems. Use a face shield, safety glasses, hearing protection, and gloves that fit. Avoid loose sleeves. Tie back hair.
Check the wheel for cracks, chips, or moisture. Ring-test only if your site procedure allows it and you are trained. If in doubt, mount a new wheel. A $4 disc is not worth a hospital visit.
Simple. But simple is not the same as optional.
Step 5: Mark, support, and clamp
Mark the cut line clearly. Support both sides of the cut so the material does not pinch the wheel. Clamp the workpiece to a stable surface. Never hold it with one hand and cut with the other.
For long extrusions, support the offcut. If it drops, it can bind the wheel. That bind can kick back. In my experience, kickback is usually a support problem before it is a wheel problem.
Step 6: Make the cut with light pressure
Let the wheel do the work. Start the grinder, let it reach full speed, then enter the cut at the marked line. Use light, steady pressure. Do not twist the grinder. Do not plunge. Do not force the cut to go faster.
If the aluminum starts to load the wheel, stop. Let it cool. Clean the wheel if the manufacturer allows it. Switch to a wheel designed for aluminum if needed. Forcing a loaded wheel is how you get heat, smoke, and a bad finish.
The vendor is 'flexible.' What I mean is they will promise a fast delivery, but the wrong disc still shows up if the PO does not specify the application.
Step 7: Deburr, inspect, and document
After the cut, deburr the edge. Use a file, a deburring tool, or a Norton Abrasives polerpad for blending if the finish matters. Inspect the cut for heat discoloration, cracks, or a rough edge that will fail inspection later.
Then document what was used. Wheel type, RPM rating, grinder, operator, and job number. This sounds like paperwork. It is also how you stop the same mistake from happening next month.
We’ve processed maybe 180 MRO orders for the shop. Maybe 160, I’d have to check. The ones with good notes are the ones we can repeat.
Procurement notes most people ignore
Here is the part that is specific to admin buyers. You can follow every cutting step and still create a problem if the purchasing side is sloppy.
First, do not buy abrasives only by unit price. The lowest quote often has hidden costs: wrong spec, slow delivery, no invoice, no lot traceability, or a wheel that loads after three cuts. To be fair, budgets are real. I get why people chase the cheapest option. But the hidden costs add up.
Second, verify invoicing and traceability before you approve a new vendor. In 2021, I found a great price from a new supplier—about $600 cheaper than our regular source. Ordered 200 discs. They could not provide a proper invoice, only a handwritten receipt. Finance rejected the expense report. I ate $600 out of the department budget. Now I verify invoicing capability before placing any order.
Third, standardize the common SKUs but keep the application notes. A bi- metal hole saw set cmah1set7 and a grinding wheel 71897 may both be valid MRO items, but they solve different problems. If your purchasing system only lists a price and a product name, your shop will eventually use the wrong item.
Personally, I would rather pay 15% more for a disc that matches the job than save 15% and pay for rework. That is not a universal rule. It is a TCO argument. Rework, downtime, and safety incidents cost more than the difference in most B2B abrasive orders.
Common mistakes and cautions
- Using a ferrous metal grinding wheel on aluminum without checking the manufacturer’s guidance.
- Ignoring the max RPM printed on the wheel.
- Removing the guard or using the wrong wheel size.
- Cutting without clamping or supporting the offcut.
- Buying the cheapest disc and assuming it will perform like a specified abrasive.
- Skipping PPE because the cut is 'quick.'
- Ordering by product name only, without alloy, thickness, RPM, or application notes.
Check your tool manual, the abrasive manufacturer’s application data, and your site safety procedure. OSHA 29 CFR 1910.215 and ANSI B7.1 are starting points, not a substitute for training. Verify current requirements as of January 2025.
If you are responsible for how to cut aluminum with angle grinder work in a shop, make the checklist part of the PO. It is less exciting than a new tool. It is also cheaper than a rework ticket.
Leila Farzan
Leila Farzan is an independent welding, abrasives, and cutting accessories analyst covering welders, electrodes, wire, grinding wheels, flap discs, cutting discs, drill bits, saw blades, hole saws, and router bits. She references ISO 525 abrasive-product dimensions and ISO 9606-1 welding qualification concepts while examining wheel speed, grit, bond, electrode class, duty cycle, kerf, tooth geometry, and material compatibility. Her guides help fabricators choose consumables, control process risk, and compare cut or weld quality.