-
The Spec Sheet Won't Save Your Fingers
-
Argument 1: The Price Per Wheel Is the Wrong Number
-
Argument 2: The Speed Rating Isn't a Suggestion
-
Argument 3: The "Good Enough" Wheel Is a False Economy—Until It Isn't
-
The Counterargument: "We Can't Afford Premium on Every Order"
-
Bottom Line: Safety Starts at the Quote
The Spec Sheet Won't Save Your Fingers
Here's my opinion, and I'll defend it: most angle grinder injuries don't happen because someone skipped the face shield. They happen because someone bought the wrong wheel, mounted it on the wrong tool, and ran it at the wrong speed. The PPE is step six. The wheel selection is step one—and almost nobody treats it that way.
I coordinate emergency supply orders for industrial clients. Last quarter alone, my team handled 47 rush jobs—everything from a fab shop that blew through its flap disc inventory mid-shift to a contractor who needed a bi-metal saw blade set 11-pack on a Friday afternoon because the job site was three hours from the nearest supply house. I've seen what happens when a wheel fails. I've also seen what happens when a buyer saves $0.40 per wheel and loses a $12,000 job because the cut quality was garbage.
So let me walk through what actually matters—and why the price tag at the bottom of the quote is lying to you.
Argument 1: The Price Per Wheel Is the Wrong Number
Most buyers focus on per-unit pricing and completely miss the cost-per-cut. That's the outer-layer cost—the one that shows up in labor hours, rework, and downtime. A $3 wheel that lasts 20 cuts costs you $0.15 per cut. A $1.80 wheel that lasts 6 cuts costs you $0.30 per cut. Guess which one the purchasing spreadsheet flags as "cheaper."
I had a client—a mid-size metal fabrication shop in Worcester, MA area—that switched abrasive suppliers to save 22% on unit cost. Three weeks later, their operators were changing wheels twice as often. We calculated it out: the "savings" cost them an extra 1.7 labor hours per shift in wheel changes alone. At $38/hour loaded labor, that's $64.60 per shift in hidden cost. On a two-shift operation, that's over $2,500 a month evaporating because someone liked a lower line item.
The question everyone asks is "what's your best price?" The question they should ask is "what's the expected cut count per wheel, and what's the variance?" If the vendor can't answer that second question with data, that's your first red flag.
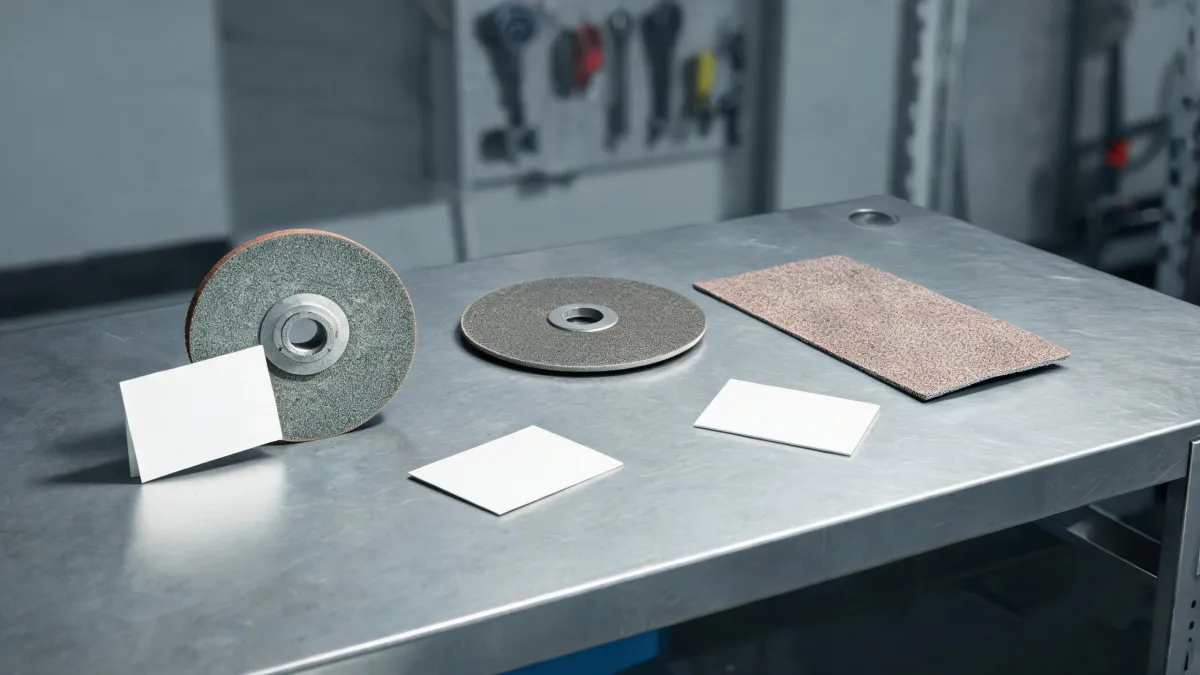
This is where brand-backed product lines matter. Norton Abrasives, for example, publishes performance data by application—not just a single "up to" number. That's the difference between a spec you can plan around and a spec that's basically marketing. When you're comparing Norton abrasives F240 or a Norton rightcut wheel against a no-name alternative, the relevant comparison isn't price per unit. It's price per documented outcome.
Argument 2: The Speed Rating Isn't a Suggestion
Here's a number that should be tattooed on every grinder: maximum RPM.
Every wheel has one. Every grinder has an operating speed. If the wheel's max RPM is lower than the grinder's no-load RPM, you've built a fragmentation grenade. This is not theoretical—it's the root cause behind a huge share of grinder incidents. And it's an easy check. It takes five seconds. Yet in rush situations, I've watched people grab whatever wheel is closest because the clock is ticking.
Had two hours to decide on a replacement order last month. Normally I'd verify the full spec sheet with the vendor, but there was no time. Went with our usual line based on trust alone. Turns out the batch had a different backing formulation—same part number, new supplier facility. The wheels ran fine, but three of them wobbled noticeably at speed. Not ideal, but workable. We flagged it, documented it, and now we require a first-article check on every new batch.
Point is: even when you do everything right, sourcing changes happen. The spec sheet is your contract. Read it every time.
Argument 3: The "Good Enough" Wheel Is a False Economy—Until It Isn't
Now, I'm not going to sit here and tell you that premium abrasives are always the answer. That would be dishonest, and it's the kind of blanket statement that makes procurement teams stop listening.
There's a real case for budget wheels on low-duty, non-critical work. Deburring a few pieces on a bench grinder? A mid-tier wheel is fine. Cutting rebar on a job site where the operator is experienced and the volume is low? You don't need a premium ceramic. Simple.
But here's the surprise: the flip side is more common than people think. I've seen shops buy premium wheels and use them wrong—wrong angle, wrong pressure, wrong material pairing—and then blame the product. A $12 ceramic flap disc destroyed in four minutes because someone leaned into it like it was a grinding wheel. That's not a product failure. That's a training gap masquerading as a procurement problem.
The legacy myth here is: "Expensive wheels are wasted on rough work." That thinking comes from an era when abrasive formulations were less specialized. Today, a wheel engineered for mild steel will underperform on stainless—and vice versa. The "expensive" wheel isn't expensive if it's the right wheel. It's just correctly priced for the job.
The Counterargument: "We Can't Afford Premium on Every Order"
Fair. You can't. And you shouldn't try.
What you can do—what I'd argue you must do—is match the wheel to the risk. High-volume production cuts on expensive material? Premium. One-off maintenance work on mild steel? Mid-range is defensible. Emergency order at 4 PM on a Friday? You pay for availability, not for the brand name. That's just reality.
"After three failed rush orders with discount vendors, we now only use suppliers who publish cut-rate data and hold inventory in our region. The extra 8-12% on unit cost is insurance."
That's not a quote from a trade magazine. That's our actual internal policy, implemented after a 2023 incident where a $900 rush order of cut-off wheels arrived with the wrong arbor size—48 hours before a client's shutdown window. We paid $800 extra in expedited freight to get the right parts. The project was saved. The lesson wasn't.
So when someone tells you transparency in pricing is just a feel-good marketing angle—no. It's an operational advantage. The vendor who lists what's not included, who tells you the lead time before you ask, who flags the spec difference between the F240 and the standard line—that vendor is worth 10% more because they're eliminating the 40% risk of a scramble.
Bottom Line: Safety Starts at the Quote
How to safely use an angle grinder? Wear your PPE. Sure. Check the guard. Yes. Match the wheel to the RPM. Absolutely.
But before any of that, buy from someone who tells you what you're actually getting. Ask for the cut-rate data. Ask what's not included. Ask whether the bi-metal saw blade set 11-pack you're ordering is rated for the material you're cutting—because "bi-metal" covers a lot of ground, and the wrong tooth count will cost you more than the price difference.
And if a supplier can't answer those questions? That's not a discount. That's a hidden fee waiting to happen.
Transparency isn't a courtesy. It's the cheapest safety feature you'll ever buy.
Darius Campbell
Darius Campbell is an independent power tool and cordless systems analyst covering drills, impact drivers, impact wrenches, grinders, circular saws, rotary hammers, and jigsaws. He uses IEC 62841-1 safety requirements while comparing rated input, battery voltage, torque, no-load speed, duty cycle, vibration, dust control, runtime, and accessory compatibility. His evaluation articles help contractors and buyers match tool platforms to workload, mobility, service conditions, and total battery-system cost.