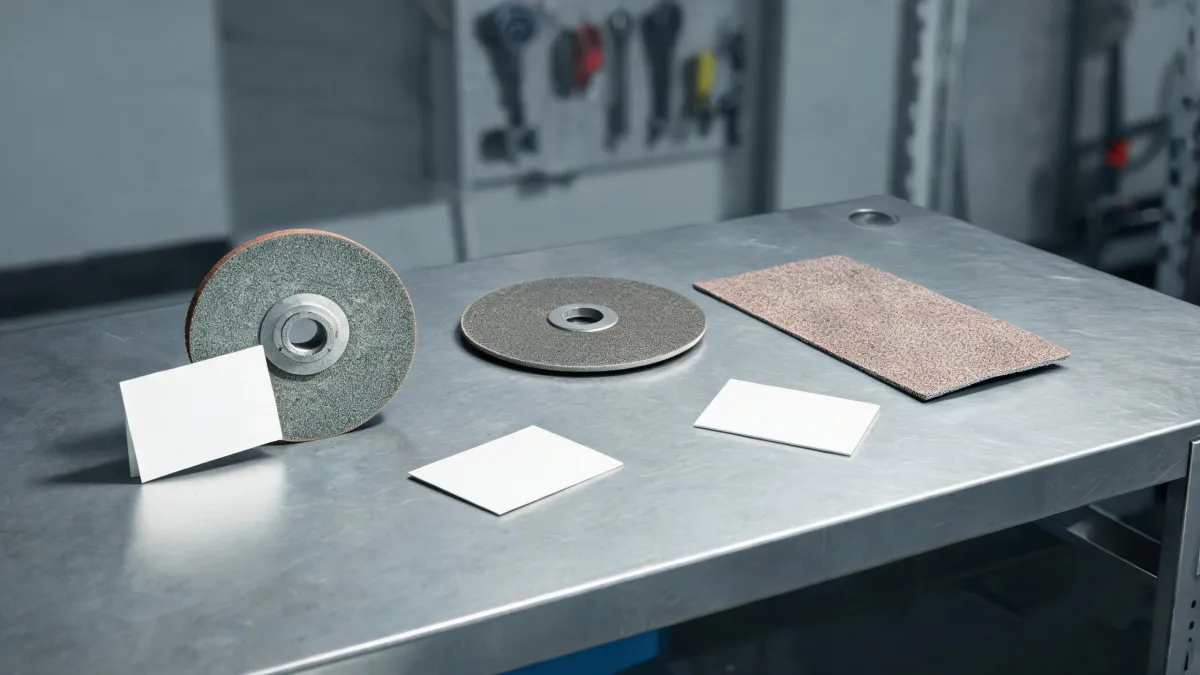
I manage purchasing for a 40-person maintenance and repair shop. That means I handle every order for abrasives, cutting tools, and supplies—roughly $60k a year across 8 vendors. I'm not the person running the grinder every day, but I'm the one who hears about it when the grinder doesn't work. And in the past few years, I've learned something that surprised me.
Most grinding wheel problems are not the wheel's fault. The real culprit is something called dressing, and it's often ignored until the wheel gets thrown in the trash.
The surface problem: wheels that "won't cut"
Last spring, a technician dropped a grinding wheel on my desk. It looked fine. Still had plenty of abrasive left. But he said it had stopped cutting steel. It just glided over the surface and sparked without removing material.
I did what a lot of buyers do: I blamed the product. I considered switching vendors. I even checked whether our new shipment was defective. Then someone in the shop asked a simple question: when was the last time that wheel was dressed? I didn't know.
That's the surface problem. A grinding wheel feels dead. It creates friction, heat, and noise. The natural instinct is to replace it. But in many cases, the wheel is not dead. It's just loaded or glazed. And the fix takes less time than walking to the stockroom.
What is dressing a grinding wheel?
Let's answer the core question directly. Dressing a grinding wheel means using a dressing tool to remove the dulled abrasive grains and the material that has become embedded in the wheel's surface. Or rather, it clears the loaded surface and exposes fresh, sharp grains, which restores the wheel's cutting action.
It's not the same as truing, which is about making the wheel round and concentric. You can true a wheel without dressing it, and you can dress a wheel without fully truing it. In a normal shop, dressing is the one that matters most day to day.
Here's something vendors won't tell you: they make more money when you replace wheels than when you dress them. If you aren't buying dressing sticks, you'll replace wheels more often. That's good for their numbers, not for your maintenance budget.
I still kick myself for the months we spent blaming a vendor for wheels that didn't cut. We threw away at least 80 wheels before I looked up what dressing meant. At $18 to $35 a wheel, that was real money. Actually, it was closer to $1,500 if you count the labor too. And a dressing stick costs about $12.
The deep cause: it's usually not what you think
Once the wheel is dressed, the next question is why it loaded or glazed in the first place. In our shop, three things cause most of the premature failures.
Wrong abrasive for the material
Aluminum is the classic example. Soft materials like aluminum, brass, and certain castings load up a conventional grinding wheel almost immediately. The metal fills the spaces between the abrasive grains, and the wheel loses its bite. It looks like the wheel is worn out, but the grains are still sharp underneath the clogged layer.
One of our maintenance jobs involved refurbishing an aluminum single wheel vintage caster. It's a small job, but the tech went through three grinding discs and said the material was awful. The real issue was that aluminum was loading the wheel. Dressing it between passes made the same disc last for the whole job.
The same logic applies to a metal saw blade. A blade that doesn't cut cleanly isn't always dull. Often it's loaded with material or has developed a glazed edge from excessive heat. Replacing it is one option, but sharpening or dressing it is cheaper—and it works.
Wrong grit size and the F240 confusion
Grit size is another hidden problem. I once saw a purchase request for Norton Abrasives F240, and the technician said it was for heavy grinding. F240 is a very fine grit. It's used for polishing and finishing, not for stock removal. If you use a fine grit for a coarse job, it glazes immediately and creates heat.
That's not a product defect. That's a matching problem. Coarse work needs coarse grit. Fine work needs fine grit. And if the wheel is already dull, dressing it first matters more than the grit number.
I also get requests for Norton Abrasives trekant slipemateriell—that's the Norwegian term for triangular sanding material. It's a great product for detail work and corners. But it's a sanding aid, not a replacement for dressing a grinding wheel. Right tool, right job.
What skipping dressing actually costs
The most frustrating part is that the fix is so cheap. You'd think a $12 dressing stick would be standard equipment in every shop, but it's often the last thing anyone orders.
Let's run the math. If you throw away a $25 wheel because it's loaded, that's bad. But the bigger cost is labor. A tech who stops a job, walks to the stockroom, gets a new wheel, mounts it, and re-aligns the work has lost 10 to 15 minutes. In a shop with multiple grinders, that adds up by the end of the day.
Quality suffers too. A glazed wheel doesn't cut; it burns. On steel, that means discolored edges and poor surface finish. On softer metal like an aluminum single wheel vintage caster, it means the part gets hot enough to deform. The work has to be redone. A 5-minute dressing step would have prevented the rework.
In our 2024 vendor consolidation project, we added a simple rule: every grinding station gets a dressing stick, and every wheel gets dressed at the first sign of loading. That one change cut our abrasive spending by about 22% in the first year. We didn't buy cheaper wheels. We bought fewer wheels because the ones we had actually kept cutting.
The simple fix: dress first, replace later
Dressing isn't complicated. Here's the routine that works for us:
- Check the wheel before mounting. Cracks, chips, or an out-of-round wheel should be replaced, not dressed. The ANSI B7.1 standard on the use, care, and protection of abrasive wheels is a good reference for this.
- Dress at the first sign that the wheel is smooth, glazed, or slow to cut. Don't wait until it's completely buried in the material.
- Use the right dressing tool. A dressing stick for general work, or a diamond dresser if you need precision and flatness.
- Replace the wheel when it's worn down to the minimum size printed on the wheel, or if it won't run true after truing.
That's it. The hard part isn't the technique. It's making the habit. In my experience, a checklist is the cheapest insurance you'll ever buy.
Five minutes of verification beats five days of correction.
When you actually need a new wheel
Dressing doesn't fix everything. If the wheel is below the minimum diameter, cracked, or out of balance, replace it. If it's the wrong type for the material, a replacement may be justified. But the default answer should be to dress it first.
I can only speak to our operation: 40 people, standard industrial abrasives, predictable maintenance and repair work. If you're grinding exotic alloys or doing precision aerospace work, the tolerances are different and your dressing procedure should be more rigorous. But the principle is the same.
Bottom line
When someone asks what is dressing a grinding wheel, the short answer is: it's how you bring a grinding wheel back to life. Before you order more Norton Abrasives wheels, make sure you're also ordering dressing equipment and using it.
If you're dealing with fine finishing, look for Norton Abrasives F240 for the correct grit. If you need triangular sanding material for detail work, Norton Abrasives trekant slipemateriell is available for that. But neither of those will help an undressed grinding wheel.
And if you're restoring an aluminum single wheel vintage caster or cutting with a metal saw blade, remember the same lesson: the tool probably isn't dead. It's just loaded. Dress it, and let it keep working.
Maren Jorgensen
Maren Jorgensen is an independent hand tool and torque applications analyst covering wrenches, pliers, screwdrivers, hammers, sockets, ratchets, hex keys, and tool sets. She applies ISO 6789-1 torque-tool conformance principles while examining jaw capacity, leverage, fastener engagement, torque range, accuracy, handle geometry, and material hardness. Her practical guides help tradespeople and procurement teams select suitable tools, plan controlled tightening, and compare durability without relying on brand reputation alone.