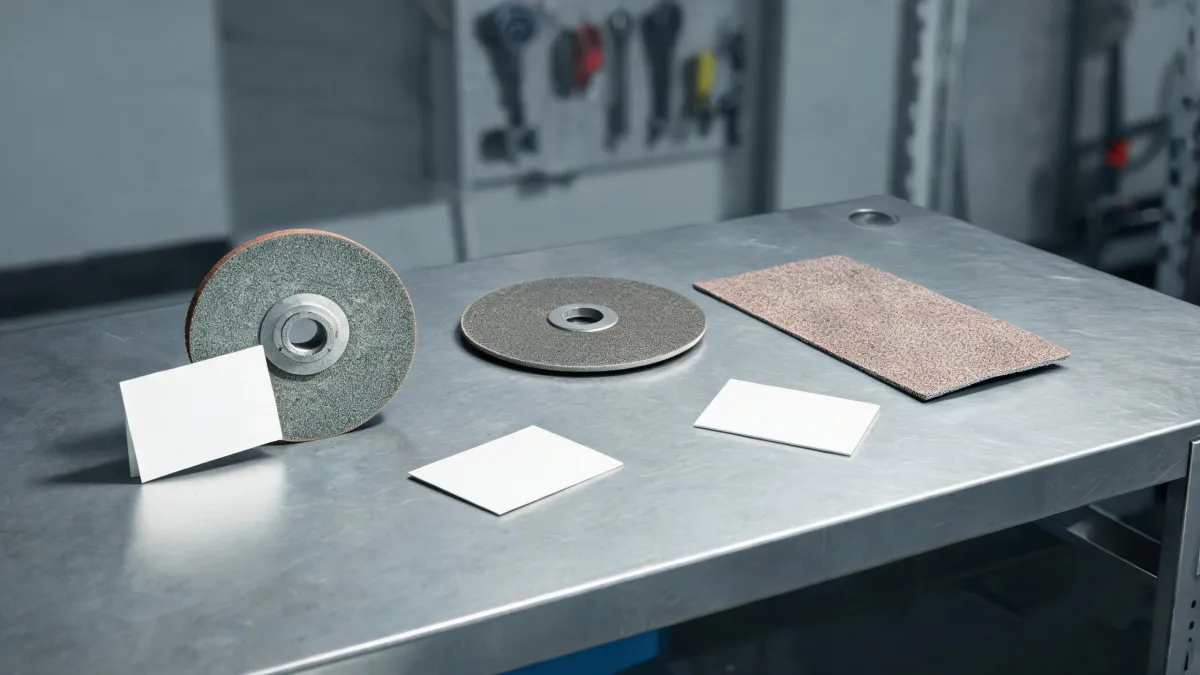
Let's start with a scene I've watched play out more times than I can count.
You're finishing a weld on a railing, using an angle grinder with a fresh flap disc. The surface looks clean. You sign off on the job. Then the inspector walks over, runs a fingernail across the weld, and shakes his head. 'Not acceptable.'
Your first instinct is to blame the grinder. Or the operator. Or the inspector.
But in my seat—quality review on industrial supply orders—the real culprit is almost always upstream. It's the consumables. And the small decisions nobody writes down.
Searching 'what is an angle grinder used to grind nccer' only gets you halfway
I'm a quality/compliance manager at an industrial supply company. I review every deliverable before it reaches customers—roughly 200 product lines a year. In our Q1 2024 audit, 14 of 47 first deliveries had at least one spec discrepancy. Most were 'minor': wrong grit, wrong fastener, wrong package size. But minor discrepancies cause real job-site failures.
Search 'what is an angle grinder used to grind nccer' and you'll get the textbook list: grinding welds, removing rust, surface prep. That's all true, but it skips the hardest part: choosing consumables that won't sabotage the tool. NCCER's power tools module teaches you the operation, not the supply chain behind it.
Deeper cause: F240 is not a color
Here's something vendors won't tell you: grit numbers are averages, not exact diameters. Two boxes marked 'fine grit' can behave completely differently depending on who made them.
Take the product code 'Norton Abrasives F240.' F240 is a FEPA F-series grain size, roughly 58 microns. It's a fine finish grain. But when a P.O. says 'Norton Abrasives F240,' it's not just a grit number—it's a controlled grain distribution. The Norton Abrasives Worcester MA legacy isn't a nostalgic brochure line; it's why a brand spec like this has decades of testing behind it.
What most people don't realize is that a no-name F240 substitute might have the same nominal grit, but a wider bell curve. Some grains are too coarse, leaving scratches. Some are too fine, causing burnishing instead of cutting. The operator blames himself. The inspector blames the operator. And the real problem is a spec that was substituted without anyone asking.
I've rejected batches where the brand wasn't specified, because 'equivalent' doesn't mean 'same.' If you don't specify that level of consistency, you're gambling with your finish.
The fastener side of the same problem
Angle grinder work doesn't happen in a vacuum. You're mounting a guard. You're attaching a handle. You're using a grinding wheel rated for a certain RPM. If you ignore the fasteners, you're creating a secondary failure.
A perfect example: using a #10 x socket hex-drive sheet metal screw where a metal lock nut belongs. I see this on light-gauge metal assemblies all the time. The socket hex drive is nice because it resists cam-out. The screw is fine for thin sheet metal. But it's not a vibration-resistant fastening system on its own.
A metal lock nut is a one-piece prevailing torque nut. It doesn't need a nylon insert; it deforms slightly as it seats, which grips the threads. But—and here's the insider detail—it's not unlimited reuse. After a few cycles, all-metal lock nuts lose their prevailing torque. If you reuse them, you might as well use a plain nut.
The quality problem is not that people use the wrong part. It's that they don't know which problem they're solving. Sheet-metal screw vs. through-bolt and lock nut are different solutions to different loads. Mixing them up on an angle grinder guard—where vibration is guaranteed—is how parts become projectiles.
The small-order trap
Now we get to the part that gets under my skin.
In my first year, I made the classic specification error: I assumed 'standard' meant the same thing to every vendor. Cost me a $600 redo and a week of schedule. I've also watched a contractor get told 'we don't do a 25-box order' by one distributor, only to get the same product shipped from a bigger one in two days.
The old 'local is always faster' thinking comes from an era before modern logistics. Today, a well-organized supplier with inventory visibility can beat a disorganized local stockroom. And the 'small customer is a hassle' attitude is a red flag, not a law of nature.
Small orders are how contractors test a new abrasive before committing to a pallet. If a supplier treats a modest first order like an inconvenience, they're telling you what the relationship will feel like when something fails. When a one-man shop needs a box of Norton Abrasives F240 discs by Friday, the answer should be 'yes, here's how,' not 'that's below our minimum.'
What this really costs
I'd rather know about a bad abrasive in the receiving area than on the jobsite. But when spec confusion slips through, the cost is never just the price of the disc or the screw.
Here's a concrete example. We had a project that needed fasteners on a high-vibration enclosure. The drawings called for through-bolts with a metal lock nut. The order got 'simplified' to #10 x socket hex-drive sheet metal screws because someone thought screws and bolts were interchangeable. 80 enclosures went out the door. Nine came back within a month because the screws backed out. The rework cost was $18,000 plus lost goodwill.
I've also done it myself. Skipped the final review because we were rushing and 'it's basically the same as last time.' It wasn't. $400 mistake.
That was not a failure of the screw. It was a failure of the decision process. And the same logic applies to abrasives. Wrong grit, wrong bond, wrong backing—these are not minor details. On a grinding wheel, wrong speed ratings are a safety issue. ANSI B7.1 exists for a reason.
The fix is boring, and that's the point
Solutions don't need to be clever. They need to be specific.
Here's what I do on every order, and what I'd recommend for anyone buying abrasives or fasteners:
- Write the abrasive spec completely. Brand, grit system, series, and backing. 'Norton Abrasives F240' is a start. 'Norton Abrasives F240, resin-bonded, for surface prep' is better. Don't leave room for an 'equivalent.'
- Treat fasteners as safety parts. If there's vibration, use a through-bolt with a metal lock nut. If you use a sheet-metal screw, know the gauge and drive type. A #10 x socket hex-drive sheet metal screw has its place. It's just not everywhere.
- Follow the machine limits. An angle grinder is only 'simple' until a wheel fails. Wheel speed, guard, and mounting conditions are part of the spec. ANSI B7.1 covers this.
- Don't punish small orders. A single box of Norton F240 discs is a testing expense, not a nuisance. Today's 25-piece order is next year's 5,000-piece line.
That's the whole strategy. Most quality problems aren't mysteries. They're skipped details.
So next time your grinder work fails inspection, don't blame the tool. Check the abrasive, check the fastener, and check whether your supplier actually cared enough to get the small things right. The inspector will thank you.
Maren Jorgensen
Maren Jorgensen is an independent hand tool and torque applications analyst covering wrenches, pliers, screwdrivers, hammers, sockets, ratchets, hex keys, and tool sets. She applies ISO 6789-1 torque-tool conformance principles while examining jaw capacity, leverage, fastener engagement, torque range, accuracy, handle geometry, and material hardness. Her practical guides help tradespeople and procurement teams select suitable tools, plan controlled tightening, and compare durability without relying on brand reputation alone.